Global Surface Treatment Equipment & System Solutions — Since 2002

久昌机械
Get a Quote
Global Surface Treatment Equipment & System Solutions — Since 2002
久昌机械
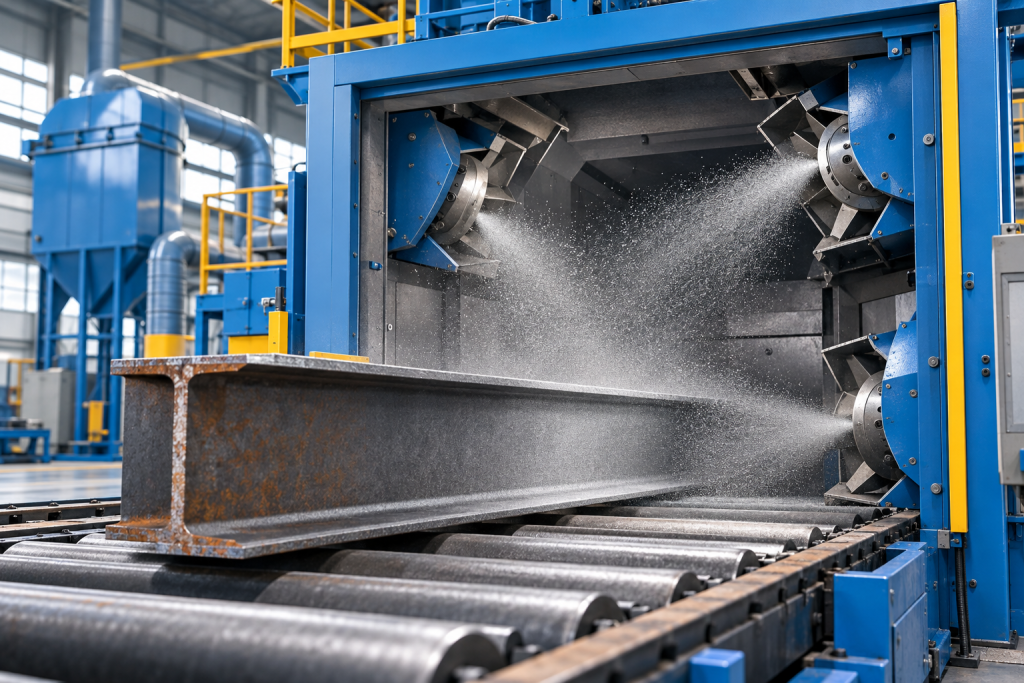
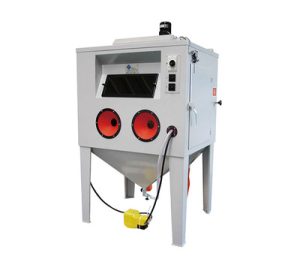
A shot blasting machine is enclosed surface-preparation equipment that propels abrasive media at a workpiece to remove rust, mill scale, sand, old coating and other surface contamination. Most industrial systems use one or more blast wheels to accelerate steel shot or steel grit. The machine then recovers, cleans and recirculates the abrasive for repeated use.
Manufacturers use shot blast equipment to prepare castings, forgings, welded structures, steel plate, profiles, pipes and fabricated assemblies. The process can clean a surface, create a controlled profile for coating, reveal defects hidden by scale or residue, and produce a more uniform appearance. The correct machine depends on the part’s size, weight, geometry, material, production volume and required finish.
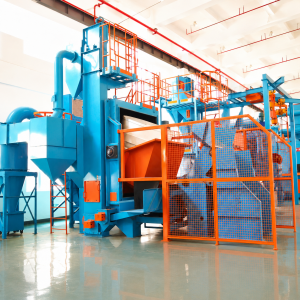
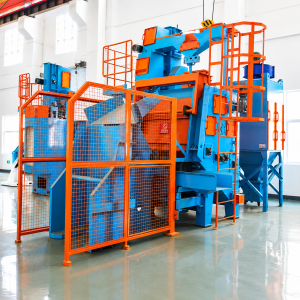
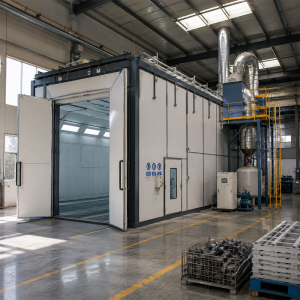
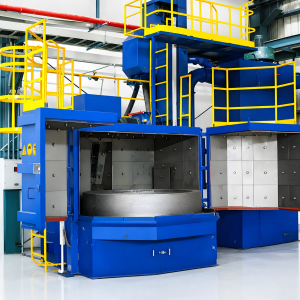
A shot blasting machine combines abrasive acceleration, workpiece handling, media recovery, separation, dust control and process control in one enclosed system. The work chamber contains the abrasive and keeps the operator away from the blast zone. A work-handling device rotates, tumbles, suspends or conveys each part so the abrasive stream reaches the required surfaces.
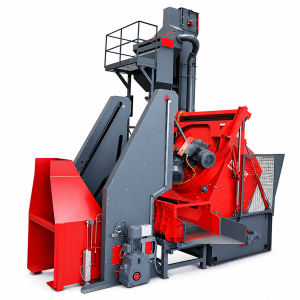
The term is often used for wheel-blast equipment. In a wheel-blast system, an electric motor turns a bladed wheel at high speed. Abrasive enters the wheel, is distributed by the control cage and impeller, and leaves the blades in a concentrated blast pattern. The pattern must be aimed at the workpiece and matched to the part movement. A poorly aligned pattern can waste energy, accelerate wear and leave shadowed areas under-cleaned.
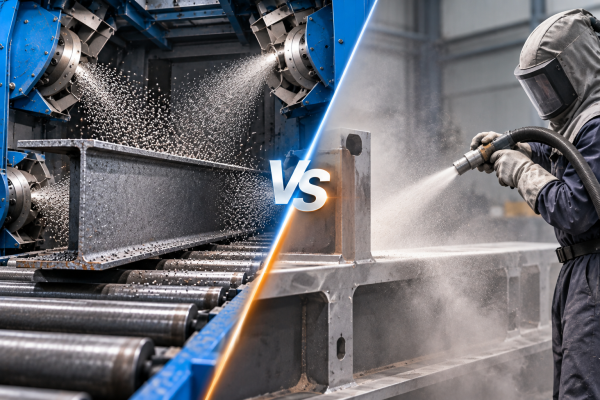
Shot blasting is related to, but different from, air blasting. Air-blast equipment uses compressed air to carry abrasive through a nozzle. It is flexible for manual work and complex or localized areas. Wheel blasting is commonly selected when parts can be handled in a repeatable path and the production goal favors automation, consistent exposure and high throughput.
Although machine layouts differ, most wheel-blast systems follow the same closed-loop sequence.
This recirculating arrangement reduces media waste, but it does not eliminate the need for process control. Operators still need to monitor media level, abrasive size distribution, wheel amperage, blast pattern, separator performance, ventilation and wear parts.
The blast wheel provides the cleaning energy. Its wheel diameter, motor power, blade design, rotational speed and abrasive flow affect cleaning intensity and coverage. Multiple wheels may be positioned around a pass-through machine so the top, bottom and sides of a workpiece are treated in one cycle.
The chamber contains the abrasive and protects the surrounding work area. Replaceable liners shield high-wear zones from direct impact. Manganese steel, alloy plates and rubber curtains may be used according to the machine design and abrasive path. Regular liner inspection prevents abrasive leakage and damage to the chamber shell.
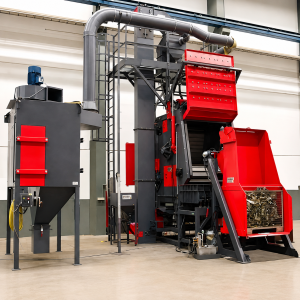
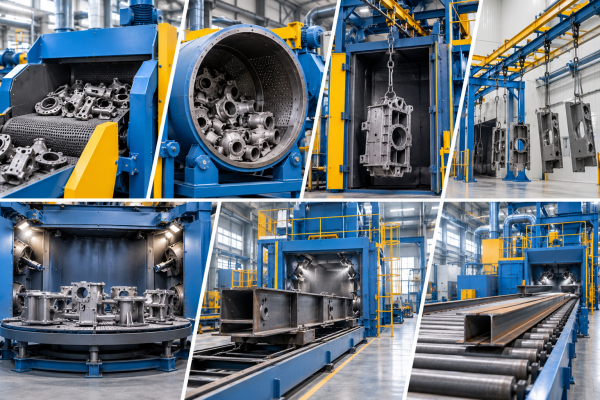
The handling system determines which parts the machine can process. Rubber tumble belts cushion smaller parts. Metal belts carry heavier or sharp-edged components. Hooks suspend irregular or delicate workpieces. Rollers move plate, profiles and pipes through the blast zone. Trolleys and turntables support large or heavy fabrications.
Screw conveyors, bucket elevators, screens and air-wash separators return usable abrasive to the hopper. Effective separation matters because fine dust reduces cleaning performance and accelerates wear, while oversized debris can block valves or damage wheel components.
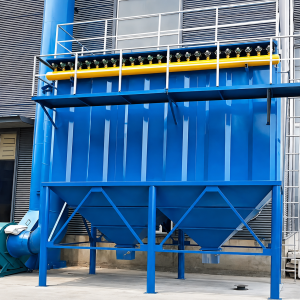
A dust collector removes fine particles generated during blasting. Correct airflow improves visibility inside the chamber, keeps abrasive cleaner and limits dust escape when doors open. Filter area, fan capacity, duct layout and maintenance access should be sized for the machine and the contamination load.
The control system coordinates loading, doors, conveyors, wheel motors, abrasive valves, elevators and dust collection. Interlocks prevent unsafe sequences. More advanced lines may store recipes, monitor motor current, track operating hours and integrate with upstream or downstream equipment.
Shot blasting does not replace every finishing process. Thin sheet can distort if impact energy is excessive. Soft metals can dent or embed abrasive. Parts with sealed cavities, narrow passages or masking requirements may need air blasting or another method. A trial using representative workpieces is the safest way to confirm finish, coverage and cycle time.
| Machine type | How parts move | Typical workpieces | Best production fit |
| Rubber tumble belt | Parts tumble on a rubber belt | Small and medium castings, forgings and hardware that can contact one another | Batch cleaning with gentler handling |
| Metal tumble belt | Parts tumble on a steel or manganese belt | Heavy, hot or sharp-edged castings and forgings | Rugged batch processing |
| Drum | Parts roll inside a rotating drum | Medium or heavy components suitable for tumbling | Simple, durable batch cleaning |
| Hook type | Parts hang from a rotating hook | Irregular, larger or impact-sensitive castings, forgings and weldments | Flexible batch production |
| Overhead conveyor | Suspended parts travel through several blast zones | Mixed suspended components and production-line parts | Continuous or indexed high-volume production |
| Roller conveyor | Parts pass through on powered rollers | Plate, structural sections, welded frames, pipe and round bar | Continuous pass-through cleaning |
| Turntable | Parts rotate on a table | Gears, flanges, flat parts and selected precision components | Controlled batch exposure |
| Trolley | A rail trolley carries the load into the chamber | Very large, long or heavy fabrications | Low-volume heavy-duty work |
Machine names describe handling style, but actual suitability depends on details such as door opening, load capacity, part envelope, number and position of wheels, abrasive flow, fixture design and unload method. Two machines with the same general name can serve very different production targets.
A supplier can recommend equipment more accurately when the inquiry describes the application, not only the desired machine name. Prepare the following information before requesting a proposal:
Representative sample testing is especially useful when a part has deep recesses, thin walls, delicate edges or an unusual coating. A trial can confirm that the selected abrasive, handling method and exposure time produce the required result without unacceptable damage.
Most wheel-blast machines are built for ferrous castings, forgings, plate, profiles, welded structures and similar metal parts. Some non-ferrous workpieces can also be processed, but abrasive selection and impact energy must be tested to avoid contamination, denting or dimensional change.
Yes, if the media, wheel power, exposure time or handling method is unsuitable. Thin sheet may distort, soft parts may dent, and precision edges may round. The machine should be selected around the most damage-sensitive feature, followed by a sample trial.
Many industrial machines can be configured to reach a near-white metal cleaning level such as Sa 2.5 on suitable steel. The result still depends on initial condition, contamination, abrasive mix, exposure, coverage and inspection method. Treat the grade as an acceptance requirement to be verified, not as an automatic result of buying a particular machine.
Yes. Wheel-blast systems normally recover and separate metallic abrasive for repeated use. New abrasive is added to replace material carried out with parts, removed by the separator or broken down during operation. Keeping a stable operating mix helps maintain finish and cycle consistency.
The best starting point is the workpiece. Send JC Blasting the material, maximum dimensions, unit or batch weight, current surface condition, required finish and target throughput. The engineering team can compare suitable handling methods and recommend a machine configuration for sample testing or quotation.
These links support the article’s topic cluster and guide readers toward relevant product pages. Add them with descriptive anchor text where they fit naturally in the published page.
Wear-resistant parts and supporting components: https://www.jcblasting.com/products/wear-resistant-parts-supporting-components/

English

Hindi

Indonesian

Russian

Spanish

Thai

Vietnamese